- This topic is empty.
-
AuthorPosts
-
2026-11-16 at 2:17 pm #15243
A hobbing gear machine is a core manufacturing solution for producing external cylindrical gears, helical gears, splines, sprockets, and other compatible toothed components through a continuous generating process. For manufacturers serving automotive, motorcycle, gearbox, pump, and power transmission markets, the machine's value depends on more than cutting speed. Gear geometry, tooth accuracy, surface finish, cycle time, tool life, and production repeatability must work together to meet the requirements of the finished component.
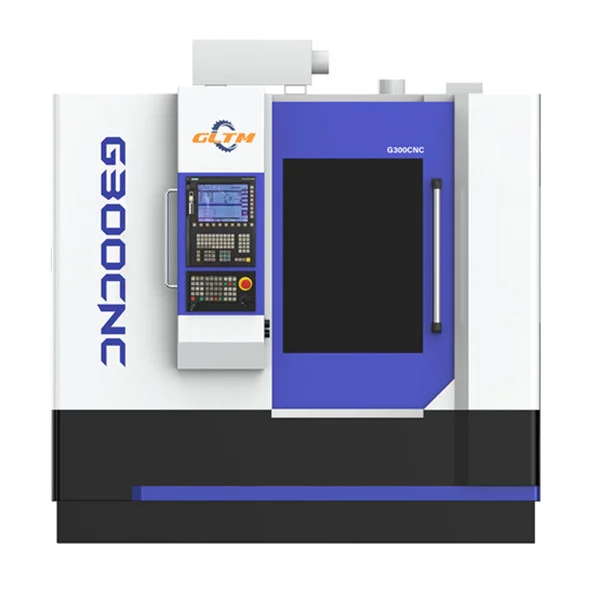
Compared with some indexing-based gear-cutting methods, gear hobbing uses a rotating hob and a synchronized workpiece to generate tooth spaces continuously. This makes it suitable for medium- and high-volume production where consistent output and efficient machining are important. However, the actual performance depends on the gear specification, workpiece material, module, helix angle, tool geometry, machine rigidity, and cutting strategy. Selecting a suitable hobbing gear machine therefore requires matching the machine's working envelope and motion capabilities to the components being produced.
Wuxi General Machinery Co., Ltd. (GLTM / GLT) has manufactured CNC gear hobbing machines since 2012. Its product range includes models from the G80CNC and G100CNC series to larger-capacity machines such as the G800CNC, G1200CNC, G1500CNC, and G2000CNC. The company also supplies other gear manufacturing equipment, supporting different stages of gear production. This range provides a basis for evaluating machine configurations against actual component dimensions, production volumes, and process requirements.
How a Hobbing Gear Machine Generates Gear Teeth
Gear hobbing is based on the generating principle. The hob is a cylindrical cutting tool with helical cutting edges, while the workpiece rotates in a coordinated relationship with the hob. As the hob and workpiece rotate, the cutting edges progressively remove material to generate the required tooth spaces.
For a conventional single-start hob, the workpiece-to-hob rotational relationship is linked to the number of teeth being generated. If the workpiece has \(Z\) teeth, one complete hob revolution corresponds to approximately \(1/Z\) of a workpiece revolution under the basic generating relationship. Multi-start hobs change this ratio according to the number of starts. In actual CNC operation, the machine also manages the required feed movements, tool positioning, and synchronization parameters.
The generating method is particularly effective for producing repeated tooth geometry because the hob's cutting edges progressively form the tooth spaces as the workpiece rotates. Unlike a process that cuts one tooth space at a time through separate indexing movements, hobbing can generate multiple tooth spaces continuously during a cutting pass. This supports efficient production when the part geometry and material are suitable for the process.
The machine's control system must maintain the required relationship between hob rotation and workpiece rotation. For helical gears, the process also requires the appropriate axial feed and coordinated angular relationship to generate the specified helix. Errors in setup, tool alignment, workholding, or synchronization can affect tooth geometry even when the machine's nominal positioning specifications appear adequate.
A suitable hobbing gear machine should therefore be evaluated through its actual gear-cutting capabilities, not simply its maximum spindle speed. The relevant parameters include the supported module range, maximum workpiece diameter, maximum workpiece width, hob dimensions, available axis movements, and permitted gear geometry. These limits must be checked against the intended part drawing before the machine is selected.
Choosing the Right Machine Size and Working Envelope
Machine capacity is one of the first factors to verify. A machine designed for small precision gears may offer advantages in compact setup and high-volume production, but it may not accommodate a large gear blank or the tooling required for a particular tooth form. Conversely, a larger machine may provide the required working envelope but involve a different investment, tooling arrangement, and production footprint.
The G-series hobbing gear machines offered by GLTM cover a broad range of nominal sizes. The specific capacity of each model must be confirmed through its technical datasheet, including the maximum workpiece diameter, maximum module, maximum cutting width, hob dimensions, and axis travel. Model numbers alone should not be interpreted as definitive specifications because machine capabilities vary by configuration.
Consider an automotive transmission supplier producing several gear families. Smaller gears may require frequent changeovers and short cycle times, while larger components may need greater fixture clearance and a larger cutting envelope. If all parts are assigned to one machine without considering these differences, setup complexity or capacity limitations can reduce production efficiency. A machine selected around the actual part family can provide a better balance between usable capacity and investment.
Module is another essential selection parameter. It describes the scale of the gear tooth system and directly influences the tooth geometry and the tooling required. The required module range must be confirmed alongside the workpiece diameter and width because a machine that accommodates the physical size of a gear may not necessarily support the required tooth specification. Internal gears also require special consideration because conventional external gear hobbing is not suitable for every internal geometry; alternative processes may be necessary.
For manufacturers producing shafts, disc gears, sprockets, or splined components, the workpiece's mounting arrangement and axial dimensions are equally important. A machine's advertised maximum diameter does not by itself establish that every component within that diameter can be machined. Tool clearance, fixture size, cutting depth, and the required feed movement must also be considered.
Machine Rigidity and Its Effect on Gear Quality
Gear quality depends on the combined behavior of the machine structure, spindle systems, workholding, hob, and cutting parameters. During machining, cutting forces can cause elastic deformation in the tool, workpiece, fixture, and machine structure. If the system lacks sufficient rigidity, these deformations may contribute to dimensional errors, surface irregularities, vibration, or inconsistent tooth profiles.
GLTM describes its machine structures as using double-wall and high-rib plate designs, with finite element analysis applied to structural design. The engineering objective is to balance overall rigidity with machine stability. Structural analysis can help identify areas of high stress or deformation during the design stage, but finished-machine performance must still be established through actual machining tests and inspection.
Workholding is also critical. A gear blank that is not clamped securely can shift or vibrate under cutting forces, while an unsuitable fixture may introduce runout or alignment errors. For shaft gears, the support arrangement must control deflection over the workpiece length. For disc gears, the fixture must provide stable positioning without obstructing the hob's cutting path.
The machine's rigidity should be evaluated in relation to the material, module, cutting depth, and required production rate. A process designed for high material removal may impose different dynamic loads from a finishing pass. In either case, increasing cutting speed without maintaining suitable rigidity and damping can worsen vibration and reduce tool life.
A useful acceptance test includes machining a representative workpiece under the intended production conditions. The resulting gear should be measured for the specified tooth geometry, pitch-related characteristics, runout, and surface quality using appropriate inspection equipment. This is more meaningful than evaluating machine structure or spindle speed in isolation.
CNC Control and Process Repeatability
CNC control allows the machine to coordinate the hob spindle, workpiece spindle, and required feed axes according to the selected gear geometry and machining strategy. Compared with manual operation, a well-configured CNC system can reduce repetitive setup adjustments and make production parameters easier to reproduce across batches.
However, CNC capability does not automatically guarantee gear accuracy. Repeatability depends on mechanical condition, axis synchronization, backlash compensation where applicable, thermal stability, tool condition, workpiece clamping, and the correctness of the machining program. The operator must also select suitable cutting parameters for the material and required quality level.
For high-volume production, consistent setup documentation is particularly valuable. Recording the hob specification, workpiece material, cutting parameters, fixture configuration, and inspection results helps establish a repeatable process. If a quality deviation occurs, these records provide a starting point for identifying whether the cause is tool wear, setup variation, material inconsistency, or a machine-related issue.
A manufacturer should also consider how easily the machine integrates into the existing production line. Relevant factors include the CNC interface, program management, setup procedures, workpiece loading method, chip evacuation, coolant arrangements, and the availability of maintenance support. Automation may reduce manual handling, but only if the machine's operating cycle, workholding, and material flow are designed to support it.
Cutting Tools, Parameters, and Tool Life
The hob is a major factor in gear hobbing performance. Its geometry, material, coating, number of starts, and condition influence cutting forces, surface finish, achievable production rate, and tool life. The tool must match the gear specification and the workpiece material, while the cutting strategy must account for the machine's available power, rigidity, and speed range.
Cutting speed and feed rate should be selected according to the tool manufacturer's recommendations and validated machining conditions. Higher cutting speeds may reduce cycle time but can also increase thermal loading and tool wear. Excessive feed can increase cutting forces or degrade surface quality, while overly conservative settings may limit throughput unnecessarily.
Tool wear should be monitored through a defined process rather than waiting for obvious defects to appear on finished gears. Depending on the application, useful indicators include changes in surface finish, dimensional trends, cutting noise, burr formation, and inspection results. Replacing or reconditioning tools according to a controlled schedule can reduce unexpected downtime and help maintain consistent gear quality.
Chip evacuation and coolant management also deserve attention. Chips trapped around the cutting zone can interfere with machining, damage surfaces, or complicate automated loading. Coolant selection and delivery should match the cutting process, workpiece material, and tooling requirements. These operational details can have a substantial effect on the actual production performance of a hobbing gear machine.
Quality Inspection and Production Validation
A gear's acceptance criteria depend on its application. Transmission gears, pump gears, sprockets, and other toothed components may have different requirements for tooth profile, lead, pitch, runout, backlash, and surface finish. The applicable drawing and gear quality standard should define the inspection method and acceptance limits.
A gear measuring center can provide detailed measurements of tooth geometry and help identify deviations that are difficult to assess through visual inspection alone. Other gauges and measurement systems may be suitable for particular production requirements, but the method must be capable of verifying the critical characteristics specified for the part.
Inspection should be integrated into process validation. Initial trials establish whether the machine, tooling, and cutting parameters can produce acceptable parts. Subsequent checks help determine whether the process remains stable as tools wear and production conditions change. Where appropriate, statistical process monitoring can identify dimensional drift before a large batch becomes nonconforming.
GLTM has expanded beyond gear hobbing machines into gear grinding machines, gear shaping machines, gear skiving machines, gear measuring centers, and gear chamfering machines. This broader equipment range can help manufacturers assess complementary processes where the required gear geometry, material condition, or quality specification cannot be achieved through hobbing alone.
Selecting a Hobbing Gear Machine for Long-Term Production
The right hobbing gear machine should match the required gear geometry, production volume, machining strategy, and inspection standard. Start by confirming the workpiece dimensions, module range, material, tooth form, and required quality level. Then verify machine capacity, axis configuration, spindle performance, rigidity, tooling compatibility, and the availability of technical support.
Wuxi General Machinery Co., Ltd. has developed its CNC gear hobbing machine series since 2012 and reports ISO 9001 and CE certifications, together with multiple technical patents. Its machine range serves gear-making applications across automotive, motorcycle, reducer, synchronous pulley, pump, and other industries. The appropriate model should be selected based on confirmed technical specifications and representative machining requirements rather than a general preference for a larger or faster machine.
Ultimately, a productive gear hobbing operation depends on the coordination of machine design, tooling, cutting parameters, workholding, and quality control. Evaluating these elements as one system helps manufacturers choose equipment that can produce the required gear geometry consistently, manage cycle time effectively, and support reliable long-term production.
http://www.gltmachinery.com
Wuxi General Machinery Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.