- This topic is empty.
-
AuthorPosts
-
2026-10-16 at 7:24 pm #14775
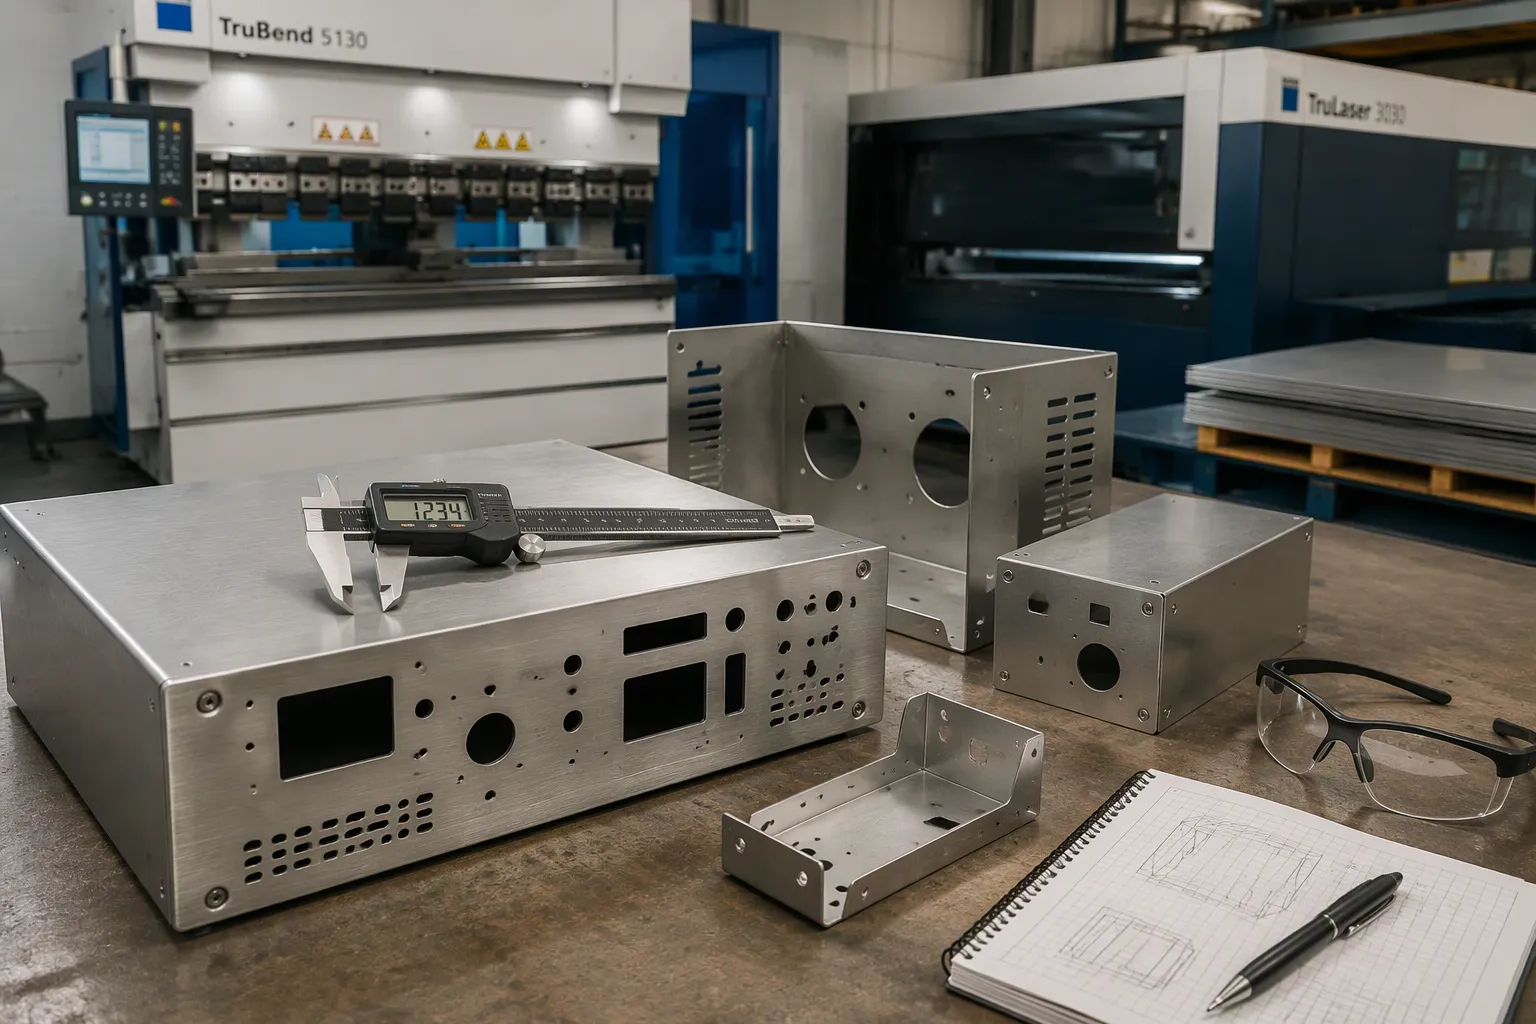
Image Source:https://www.xuxiangtaimetal.com Precision sheet metal enclosures shield sensitive equipment. They meet exact dimensional and finish requirements. Low quantity fabrication helps engineers validate designs and reach market without high-volume tooling commitments. Qingdao Xuxiangtai delivers full-cycle fabrication from design to delivery for US mechanical engineers and industrial buyers.
Key Takeaways
- Precision sheet metal enclosures protect equipment and meet exact specifications. They are essential for industries like aerospace, defense, and medical devices.
- Designing enclosures requires balancing tolerances, materials, and finishes. Over-tolerancing increases cost, while under-tolerancing causes fit problems.
- Low quantity fabrication lets engineers validate designs without expensive tooling. Processes like laser cutting and press brake bending are fast and cost-effective for small batches.
What Are Precision Sheet Metal Enclosures?
Definition and Key Characteristics
Precision sheet metal enclosures are fabricated housings that protect sensitive equipment while meeting exact dimensional and finish specifications. These enclosures serve as the physical barrier between internal components and external environments. Key characteristics include sealing for IP ratings, surface finishing for corrosion protection, and design for manufacturability.
Characteristic Description Sealing for IP Ratings Continuous sealing paths, compression gaskets, sealed cable glands, and uniform fastener spacing Surface Finishing Powder coating for steel, anodizing for aluminum, galvanization for outdoor applications Thermal Management Passive cooling via ventilation slots or active cooling with fans and heat sinks Structural Considerations Panel stiffness, material thickness based on component weight and vibration requirements Engineers achieve proper sealing by establishing continuous paths along panel interfaces, using compressible gaskets, and distributing fasteners evenly.
Common Applications Across Industries
Precision sheet metal enclosures serve diverse sectors with demanding requirements.
Industry Common Applications Aerospace Structural brackets, avionics assemblies, shielding panels Defense Electronics housings, communications enclosures, shipboard infrastructure Electric Vehicles Battery trays, module housings, power-electronics covers Data Centers Server rack frames, modular chassis, cable management systems Medical Devices Surgical instrument housings, imaging equipment enclosures Renewable Energy Solar mounting structures, inverter housings, battery storage frames Manufacturing facilities use these enclosures to protect PLCs, HMIs, and motion controllers. Food and beverage operations require hygienic stainless steel designs.
Why Precision Matters for Fit and Function
Sheet metal fabrication delivers a different tolerance profile than CNC machining. CNC turret punching achieves around ±0.1–0.2 mm tolerances for feature location on thin sheets. Laser-cut holes in mild steel up to 3 mm thick can hold ±0.1 mm tolerances with proper calibration.
Poor precision creates serious consequences. Parts may fail to fit together because of tolerance stack-ups. Tighter tolerances can increase scrap rates and costs. Delays occur when excessive inspection and rework are required.
Common Design Mistake Why It Causes Problems Better DFM Approach Tight tolerances on every dimension Forces extra setups and higher cost Identify critical dimensions and relax the rest Holes too close to bends Bending distorts holes and affects fit Keep features clear of bend areas Sharp internal corners Creates stress concentrations Add small internal radii Ignoring coating thickness Buildup affects hole sizes and fits Adjust tolerances for finishing Designing Enclosures: Tolerances, Materials, and Finishes
Designing precision sheet metal enclosures requires engineers to balance three interconnected decisions: tolerances, materials, and finishes. Each choice affects the others. A tight tolerance may demand a specific material grade. A corrosive environment may dictate both material and coating. Engineers who understand these relationships produce enclosures that fit correctly, last longer, and cost less to manufacture.
Setting Realistic Tolerances
Tolerances define the acceptable variation in a part’s dimensions. Engineers assign tolerances based on function, not habit. Over-tolerancing drives up cost because fabricators must slow production, add inspection steps, and scrap more parts. Under-tolerancing creates fit problems and field failures.
The fabrication industry recognizes three capability tiers. General or structural fabrication holds tolerances around ±1/16″ to ±1/8″ for frames and brackets. Standard sheet metal fabrication achieves ±1/32″ to ±1/16″ on formed dimensions for enclosures and panels. Precision sheet metal fabrication reaches ±0.005″ to ±0.010″ on critical cut features for electronics enclosures, medical devices, and hardware-dense designs. These tiers describe capability classes, not quality grades. Formed and assembled dimensions still require process-appropriate tolerances even in the precision tier.
Fabrication Tier Typical Tolerance Range Example Applications General or structural fabrication ±1/16″–1/8″ Frames, brackets, architectural components, structural work Standard sheet metal fabrication ±1/32″–1/16″ on formed dimensions Enclosures, panels, guards, general industrial parts Precision sheet metal fabrication ±0.005″–0.010″ on critical cut features Electronics enclosures, medical/aerospace components, EMI or environmental sealing, hardware-dense designs Individual enclosure features carry their own standard tolerances. Length, width, trim height, and inside radii typically hold ±0.015″. Nutplate positions allow ±0.030″ because they involve secondary operations. Width and length are measured at the point of tangency at the closed end of the enclosure. The open end is generally larger due to material springback and the deep draw process.
Enclosure Feature Standard Tolerance Length ±0.015″ Width ±0.015″ Trim Height ±0.015″ Inside Side Radius ±0.015″ Inside Bottom Radius ±0.015″ Nutplate Position (horizontal & vertical) ±0.030″ Two international standards govern how engineers specify tolerances. ISO 2768 defines general tolerances for linear and angular dimensions with classes f (fine), m (medium), c (coarse), and v (very coarse). A drawing note such as “Tolerances to ISO 2768-m” applies the medium class to all untoleranced dimensions. ASME Y14.5 provides the symbolic language, rules, and definitions for Geometric Dimensioning and Tolerancing (GD&T) in North America. ASME Y14.5 does not supply tolerance values. It supplies the framework for specifying geometric controls.
Feature-level tolerances depend on geometry and process. Features on the same flat surface hold ±0.005″ because laser or punch accuracy is high. Bend-to-edge dimensions allow ±0.010″ due to material thickness, bend angle, springback, and tooling. Bend-to-bend dimensions permit ±0.020″ because multiple forming operations accumulate variation. Multiple formed features may reach ±0.030″ depending on the number of bends, bend sequence, geometry, and material behavior. Tighter critical dimensions may require secondary machining, special tooling, fixtures, or additional inspection.
Feature or Dimension Typical Tolerance Primary Considerations Features on the same flat surface ±0.005″ Laser or punch accuracy, material, feature geometry Bend to edge ±0.010″ Material thickness, bend angle, springback, tooling Bend to bend ±0.020″ Multiple forming operations and accumulated variation Multiple formed features Up to approximately ±0.030″ Number of bends, bend sequence, geometry, material behavior Tighter critical dimensions Application dependent May require secondary machining, special tooling, fixtures, or additional inspection These figures are typical fabrication guidelines, not universal tolerances. Engineers must review drawing requirements and part geometry before manufacturing.
Choosing the Right Material
Material selection affects weight, strength, corrosion resistance, formability, and cost. Engineers evaluate the operating environment first, then narrow options based on mechanical requirements and budget.
Material Good Choice When Key Design Consideration 5052 Aluminum Low weight, corrosion resistance, and good formability are priorities Excellent for formed enclosures; compatible with many common finishes Cold-Rolled Steel Strength and material cost are priorities Typically requires a protective finish for corrosion resistance 304 Stainless Steel Durability and corrosion resistance are important Higher material and fabrication cost than standard steel 316 Stainless Steel Enclosure will operate in a more demanding corrosive environment Greater corrosion resistance but typically higher cost than 304 Galvanized or Pre-Plated Steel Corrosion protection is needed without post-fabrication plating Cutting, forming, and welding can affect the existing coating Enclosures are fabricated using materials like steel (including stainless steel for rust resistance), aluminum (for lightweight and corrosion resistance), and galvanized steel (for cost-efficiency and durability), with selection based on durability, corrosion resistance, conductivity, weight, and cost.
Aluminum 5052 suits most formed enclosures because it balances strength, weight, and formability. Cold-rolled steel offers an economical path when engineers add a protective finish. Stainless steel 304 handles most indoor and outdoor applications. Stainless steel 316 serves marine, chemical, and food-processing environments where chlorides and washdowns accelerate corrosion. Galvanized steel provides corrosion protection at lower cost, but fabricators must account for coating damage at cut edges and weld zones.
Selecting a Finish for Durability and Appearance
Finishes serve two purposes: protecting the base metal and shaping the product’s visual identity. Engineers select finishes based on the operating environment, expected service life, and appearance requirements.
Environment / Use Case Recommended Finish Reason Indoor office enclosure Powder coating or paint Low risk; mainly handling marks and visual consistency Outdoor electrical cabinet (humidity, UV, salt) Galvanizing + powder coat (duplex system) or anodized aluminum Corrosion cycles, UV exposure, salt in air; anodizing if weight matters Corrosive environments (chemical plants, marine, food processing washdowns) Finish becomes part of durability strategy (e.g., duplex coating, anodizing) If finish fails, part fails Production volume influences finish choice. A single prototype may use paint because it is quick, cheap, and flexible. Batches of thousands often use powder coating because it costs less per part and produces more consistent results. Electroplating offers affordable upfront costs, but long-term corrosion risk in aggressive environments can create warranty issues. Scratch- and fade-resistant finishes reduce field complaints. Easily chipped finishes create recurring service costs.
Finishing Type How It Works Common Uses Why Engineers Choose It Anodizing Electrochemical process that thickens natural oxide layer (mainly on aluminum) Electronics housings, aerospace panels, visible aluminum parts Improves corrosion resistance, adds hardness, can be dyed for color, lightweight Powder Coating Dry powder applied electrostatically, then cured in oven to form hard protective layer Outdoor enclosures, machinery frames, consumer products Durable, impact-resistant, consistent finish, wide color range, good corrosion protection Finish Durability & Appearance Strengths Limitations Powder Coating Durable, attractive finish; broad color and texture choices; good resistance to routine wear; efficient coverage across many geometries Thickness, cure temperature, and pretreatment needs; may not suit very tight fits or bare conductive surfaces Wet Paint Useful when film thickness must remain lower; specific appearance possible Primer, topcoat, and curing method must be selected for actual environment, not by color alone Plating Provides corrosion protection, conductivity, wear resistance, or specific appearance; zinc plating common for steel hardware and brackets Requires attention to dimensional buildup and material compatibility Anodizing Improves corrosion resistance and clean, durable appearance for aluminum; preserves metallic look Does not behave like a paint film; works best when base material, surface prep, and appearance expectations are defined clearly Material compatibility restricts finish options. Black oxide works on carbon steel but not stainless steel or aluminum. Anodizing applies only to aluminum. Passivation serves stainless steel exclusively. Galvanizing suits carbon steel and galvanized steel. Powder coating and painting work across nearly all metals. Engineers should verify compatibility before finalizing drawings.
Finish Carbon Steel Stainless Steel Aluminum Copper Alloys Galvanized Steel Black Oxide Yes No No No No Electroplating Yes No No Yes No Anodizing No No Yes No No Painting Yes Yes Yes Yes Yes Powder Coating Yes Yes Yes Yes Yes Galvanizing Yes No No No Yes Phosphating Yes No No No No Passivation No Yes No No No Polishing Yes Yes Yes Yes Yes Sandblasting Yes Yes Yes Yes Yes Electropolishing No Yes Yes No No Brushing Yes Yes Yes Yes Yes Environmental conditions drive finish selection. Humid or coastal installations require galvanizing or electroplating that withstands 500+ salt spray hours. Chemical exposure demands passivation or powder coating for acid resistance and solvent protection. High-temperature applications favor anodizing because it does not degrade up to 500°C.
Environmental Condition Recommended Finish Key Property Humid / Coastal Galvanizing or Electroplating Withstands 500+ salt spray hours Chemical Exposure Passivation or Powder Coating Acid resistance / solvent protection High Temperatures Anodizing Does not degrade up to 500°C Mechanical finishes offer additional options. Sandblasting removes rust, mill scale, and old coatings while giving a uniform matte finish that improves paint adhesion. Coarser grits (80-120) handle heavy removal. Finer media (220+ mesh) polish stainless steel enclosures. Electropolishing smooths metal surfaces via electric current and strengthens the natural oxide layer for improved corrosion resistance. It suits stainless steel exposed to harsh chemicals or sterilization, including FDA-compliant surfaces for pharmaceutical and semiconductor industries. Brushing produces a consistent linear or radial grain pattern that hides minor scratches and fingerprints. Automotive interior parts commonly use brushed finishes, and grain direction can be tailored as horizontal, vertical, or circular.
Surface finish influences perception. A matte black powder-coated enclosure communicates something different than a polished stainless panel. Texture, gloss level, and color consistency become part of brand identity. For consumer-facing products, surface consistency matters as much as structural strength. Even in B2B equipment, visual uniformity signals manufacturing quality. Internal brackets may prioritize corrosion resistance over appearance, while external panels may demand both. Over-finishing increases cost. Under-finishing increases risk. Consistency is often overlooked. Variations in coating thickness, gloss level, or texture create assembly mismatches and visual defects, so finishing processes must be controlled and repeatable.
Design details affect finish quality. Sharp external corners do not hold coating evenly. Slightly radiused edges behave better. Tight internal corners and deep narrow cavities are hard to coat evenly. Every coated part needs a hanging point, so engineers should design small, non-critical hanging tabs or designated contact areas. Many finishing problems are actually design oversights.
Design Best Practices for Manufacturability
Design for manufacturability (DFM) reduces cost, shortens lead times, and improves part quality. Engineers who follow established guidelines avoid common pitfalls that cause rework and delays.
- Wall Thickness — Most sheet metal enclosures use materials from 0.8 mm to 3 mm thick. Thinner sheets (~1 mm) suit consumer electronics, while thicker options are preferred in industrial settings. Keeping thickness consistent reduces fabrication errors and ensures predictable bend behavior.
- Bend Radius — A general rule is to make the inside bend radius equal to the material thickness. Tight bends can cause cracking or distortion, especially in brittle materials like stainless steel. Using a standard bend radius improves repeatability in mass production and aligns with common tooling setups.
- Mounting Points — Include features like embossed standoffs, self-clinching fasteners, or welded nuts to secure PCBs and internal components. Mounting holes should be placed away from bends and edges to prevent distortion during forming.
DFM Parameter Recommended Rule Minimum inside bend radius (cold-rolled steel, 5052-H32 aluminum) 1T for thicknesses up to 6 mm Minimum inside bend radius (304 stainless steel) 1T–2T, with 1.5T–2T recommended Minimum inside bend radius (6061-T6 aluminum) Larger radii often required Hole-to-edge distance (laser cuts) At least 1.5T Hole-to-edge distance (punched holes) At least 2T Holes under 25 mm diameter 2T plus inside bend radius from bend tangent Bend relief notch width At least 50% of material thickness Bend relief notch depth Equal to material thickness Minimum flange length (air-form tooling) 4× thickness (4T) Primary datum faces Must be flat and machinable, tolerances stated before or after finish Engineers should also address overlapping folds and fastener clearance. Provide a gap of at least 0.5 mm to 1 mm between overlapping folds to accommodate material thickness, bend radii, and minor fabrication variations. Design clearance holes 0.1 mm to 0.3 mm larger than the fastener diameter to account for punching or drilling tolerances. Reference all hole locations from a common datuming surface. Use locating tabs or alignment features to guide parts into place during assembly.
Design for sheet metal starts from a flat slab that must be bent, punched, or laser cut. Bends in one area can profoundly affect manufacturability in another. Engineers must ensure tooling access so fasteners can be reached and torqued during assembly. They should include a hole in both components to be fastened. Formed corners have a radius (a 0.030 in. / 0.76 mm inside bend radius is most common) that engineers must account for to avoid interference in the bend region. Add inside bend radii as you design and plan mating components to meet before the bend region. For U-channels, the width-to-height ratio must not exceed 2:1. Add bend relief—a slight cut where a flange meets the workpiece—to prevent deformation of the surrounding metal when forming. For ventilation, use perforation patterns (round or hexagonal, staggered) sized to achieve the needed open area. For large perforated areas, either tack weld a sheet of perforated material into the enclosure or use the smallest possible open area percentage to minimize sheet distortion.
Low Quantity Sheet Metal Fabrication Processes
Image Source: https://www.xuxiangtaimetal.com Low quantity production demands processes that avoid dedicated tooling. Engineers can validate designs, test fit and function, and reach market without committing to expensive dies.
Laser Cutting for Speed and Accuracy
Laser cutting offers flexible part geometry because it requires no dedicated hard tooling for each profile. Engineers gain freedom to create complex contours, holes, slots, and cutouts directly from digital files. A design revision needs only a program update, not a new cutting die. CNC-integrated laser cutting holds tight tolerances with minimal variation across parts and batches. The laser melts rather than cuts the material, so cut edges often need little to no deburring. Fiber lasers run continuously without operator oversight, which yields high process efficiency and lower labor costs. Prototype parts transition smoothly into production using the same digital geometry.
Bending and Forming for Small Batches
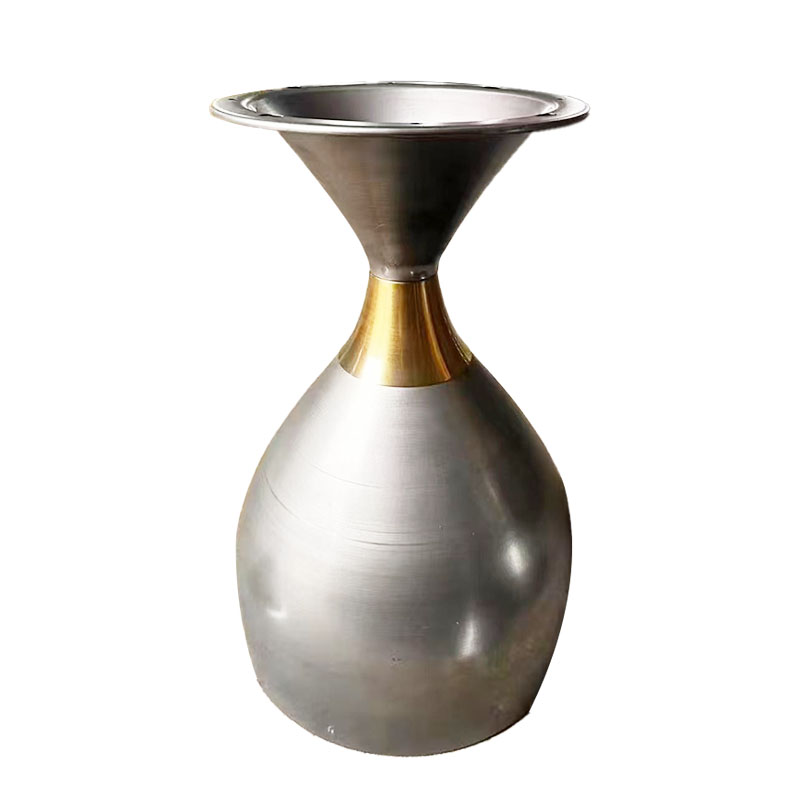
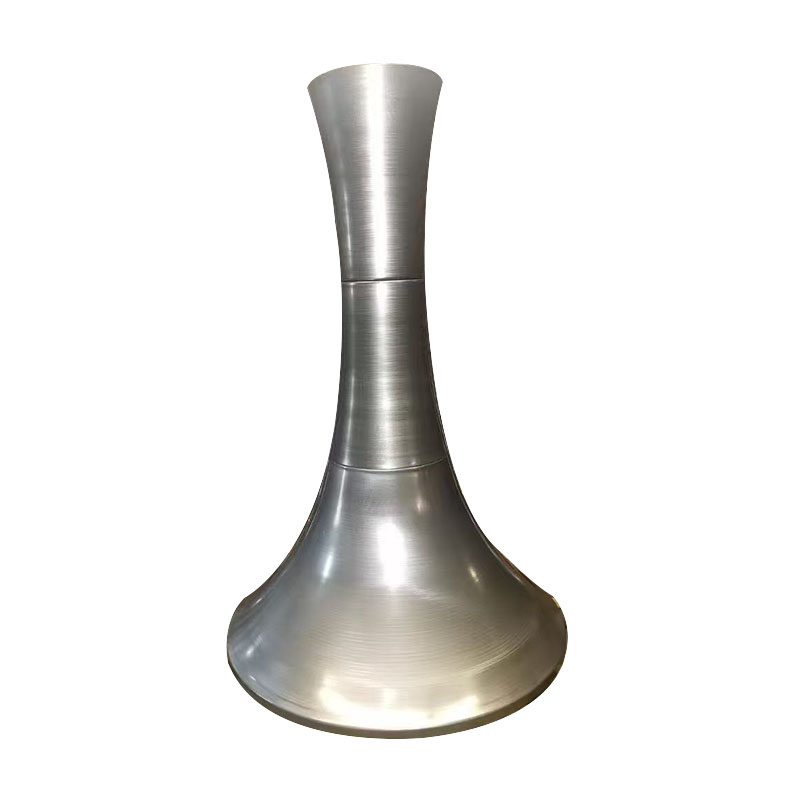
Press brakes handle small batches efficiently. A single setup can produce bends across dozens or hundreds of parts. Standard tooling covers most bend angles and radii, so engineers avoid custom die costs. For cylindrical or radial-symmetric parts, metal spinning offers a flexible alternative. It requires no costly dies and suits volumes from 10 to 500 pieces.
Welding, Riveting, and Assembly Options
Spot, arc, and laser welding create permanent bonds for structural enclosures. Riveting provides mechanical joining for non-weldable parts or where thermal distortion is a concern. Pre-riveted hardware simplifies final assembly.
When to Choose Each Process
Process selection depends on volume, geometry, and tolerance requirements.
Production Volume Recommended Process Lead Time 1–10 pcs (prototype) Waterjet/laser + press brake 7–10 days 10–50 pcs Laser + press brake 7–10 days 50–500 pcs Laser + press brake + spin/draw 10–14 days 1,000+ identical parts NC punch or stamping 1–3 weeks (die) + 2–4 days For prototype to 500 pieces, laser or waterjet cutting paired with press brake forming delivers the best balance of speed and cost. At 1,000 identical parts, NC punching or stamping breaks even on tooling costs compared to laser cutting.
Sourcing Low Quantity Parts Step by Step
Sourcing low quantity sheet metal parts follows a defined path. Each step builds on the previous one. Engineers who prepare thoroughly and evaluate suppliers systematically avoid costly delays and quality problems.
Preparing CAD Files and Documentation
A complete data package forms the foundation of every successful quote. Fabricators cannot price a job accurately without clear geometry, material specifications, and tolerance requirements. Engineers should assemble all files before contacting suppliers.
A 3D CAD file is required to generate and receive a quote. Commonly accepted file types include
.STEP,.STP,.SLDPRT,.x_t, and.IGS. The CAD-platform-neutral.STEP/.STPformat is the most typical submission choice among uploaders.CAD File Format Description Suitability for Sheet Metal Fabrication STEP (.step/.stp) Industry-standard 3D CAD exchange format that preserves solid body geometry Widely accepted by sheet metal shops; preserves precise dimensions and features, ideal for fabrication programming IGES (.iges/.igs) Older CAD exchange format supporting surface and solid models Can cause data translation errors; should be used cautiously, especially for complex parts Native CAD Files (e.g., .sldprt, .ipt, Fusion 360) Proprietary formats tied to specific CAD systems Preferred when the fabricator uses the same CAD software, as they retain full model details and metadata Surface-Only Files Files containing only surfaces without a solid body Problematic — lack thickness data needed for unfolding and fabrication; solid body should always be confirmed before sending Engineers must verify that their CAD file contains a solid body, not just surfaces. Surface-only files lack the thickness data needed for unfolding and fabrication. A quick check before submission prevents back-and-forth delays.
Documentation extends beyond the 3D model. A complete request for quote package includes several elements that fabricators need to price accurately and plan production.
Required Documentation Purpose / Details 2D drawings with dimensions and tolerances Backbone of the quote; shows size, hole locations, bend lines, weld callouts, tight vs. loose tolerances; include title block, revision level, general tolerance note; send as PDF and note any referenced specs or welding standards. 3D model (STEP or native) Fastest addition to an RFQ; enables true geometry extraction, accurate flat patterns, bend relief and hole-to-edge checks; drives laser nesting and material usage cost. Pair with drawing (model = geometry, drawing = intent). Material, grade, temper, and thickness Specify alloy, grade, temper (especially aluminum), and exact thickness/gauge; material is often the largest cost line and affects cut speed, forming, weldability, and finish. Note if substitutions are acceptable. Quantity and annual volume Provide both the quantity for this order and expected annual volume/release pattern; one-off vs. production run pricing differs dramatically due to setup, fixtures, nesting, and automation. Tolerances and critical features Flag which features are truly critical (e.g., bearing bore, bolt circle, sealing flatness); everything else can use standard shop tolerances. Over-tightening all dimensions inflates cost. Finish and special processes Include powder coating, wet paint, plating, anodizing, passivation, deburring, certifications, color/spec, masking requirements, and any cert paperwork. Delivery expectations State required date, phased release schedule, drop-ship locations, packaging, and labeling requirements to allow accurate planning and pricing. Application and part function Describe what the part does, what it mounts to, loads, and environment; this enables cost-down suggestions (e.g., combining parts, relaxing non-functional tolerances, lighter gauge). Request the missing material, geometry, tolerance, quantity, or finish information before issuing a firm quote. For a budgetary number, state each assumption and identify what could move the price.
A small batch leaves setup, programming, fixture, and finishing charges concentrated on fewer parts. Engineers who provide complete documentation help fabricators identify cost drivers early. This transparency allows both parties to discuss design adjustments that reduce expenses without compromising function.
Requesting and Comparing Quotes
Quote requests should go to multiple fabricators simultaneously. This approach provides pricing benchmarks and reveals how different suppliers interpret the same requirements. Engineers should allow adequate time for responses. Rush requests often produce incomplete quotes or premium pricing.
Comparing quotes requires more than scanning bottom-line numbers. Engineers must evaluate what each quote includes and excludes. A low price may reflect missing operations, unclear assumptions, or inferior materials.
Several factors drive cost variation between quotes. Material type, grade, and thickness represent the largest variable. Labor process and skilled work required differ by shop capability. Machine setup and configuration time affects small-batch economics. Overhead costs such as rent, utilities, and maintenance vary by region. Rush order premiums, finishing costs such as painting and powder coating, and quality standards also influence pricing.
Material costs fluctuate with market conditions. Engineers should understand current pricing trends when evaluating quotes.
Material 2024 Avg. Price ($/lb) 2025 Avg. Price ($/lb) Steel 0.50 0.67 Aluminum 1.20 1.35 Copper 3.80 4.25 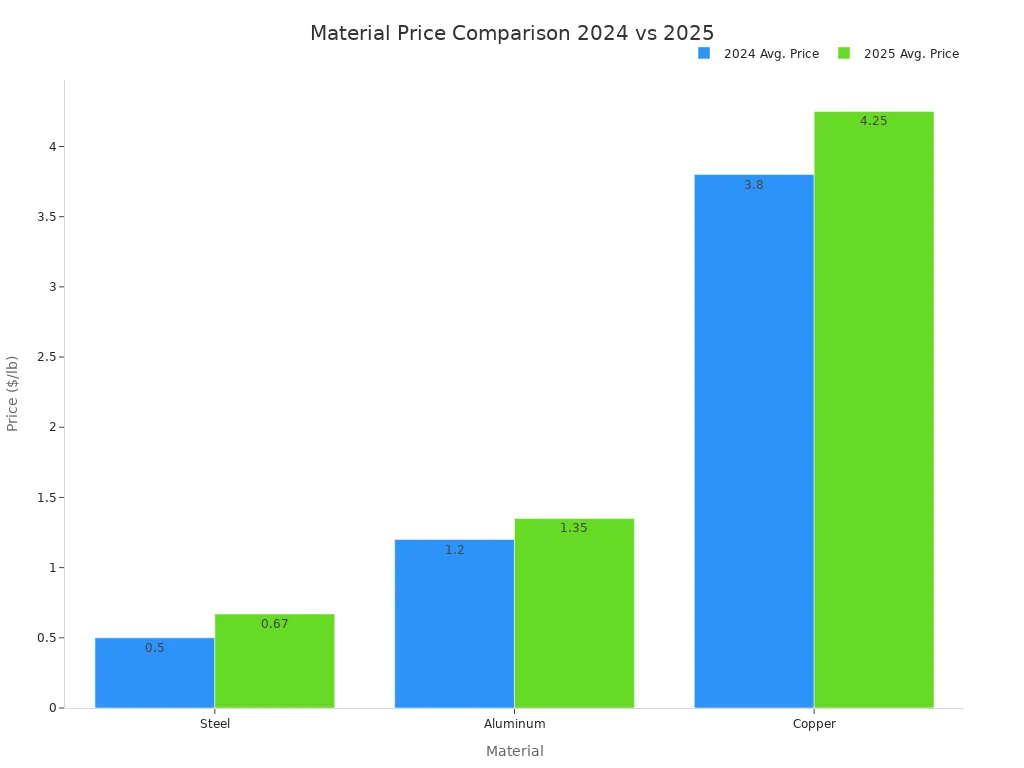
Image Source: https://www.xuxiangtaimetal.com Engineers should request line-item breakdowns from each supplier. This detail reveals how fabricators allocate costs across material, cutting, forming, finishing, and assembly. Like-for-like comparison becomes possible only when quotes share the same structure.
Key comparison factors include material costs and market volatility, labor and machine time, design complexity and tolerances, surface finishing and post-processing, quantity, lead time, and rush orders, quality assurance, certifications, and compliance, location, logistics, and delivery, and like-for-like quote comparison with detailed breakdowns.
Hidden costs deserve scrutiny. Some suppliers add fees for programming, fixturing, or minimum order quantities. Others charge separately for inspection documentation or packaging. Engineers should ask directly about any charges not explicitly listed in the quote.
Negotiation potential exists, especially for long-term partnerships. Suppliers may offer volume discounts for future orders or reduced pricing when engineers commit to release schedules. Open discussion about production forecasts often yields better terms than one-time transactional requests.
Selecting a Supplier for Small-Batch Production
Supplier selection determines project success beyond the first order. A fabricator who understands the application, communicates clearly, and maintains consistent quality becomes a valuable long-term partner. Engineers should evaluate suppliers across multiple dimensions before committing.
Certifications and quality systems provide baseline confidence. ISO 9001 represents the minimum quality management requirement for most industrial buyers. ISO 14001 demonstrates environmental compliance. TÜV CE matters for European markets. Additional certifications like ISO 13485 or IATF 16949 apply to regulated industries such as medical devices and automotive.
Manufacturing capabilities and equipment must match part requirements. Modern high-precision laser cutting handles complex geometries. Computer-controlled CNC bending ensures consistent forming. TIG, MIG, and spot welding capabilities cover most joining needs. In-house surface treatment options reduce lead times and logistical complexity.
Quality control and inspection processes reveal how seriously a supplier approaches consistency. Incoming material inspection with Mill Test Certificates (MTC) verifies material traceability. In-process inspection at each stage catches problems before they compound. Final dimensional verification confirms that finished parts meet specifications. Third-party lab testing support provides additional assurance for critical applications.
Engineering support and design for manufacturability services add significant value. Suppliers who review designs, suggest optimizations, and offer reverse engineering support can save 15-20% on total project cost. This collaborative approach benefits engineers who lack extensive sheet metal experience or who want fresh perspectives on established designs.
Communication and responsiveness separate reliable suppliers from problematic ones. Fast response times, a dedicated point of contact, transparent quoting, and clarity in answering questions all signal a well-run operation. Engineers should note how quickly suppliers respond during the quoting phase. This responsiveness often predicts communication quality during production.
Flexibility and scalability matter for growing programs. Suppliers who handle prototypes through mass production eliminate the need to qualify new vendors as volumes increase. No minimum order quantity is a key advantage for small-batch production. Engineers should confirm that a supplier can grow with their program.
Fabrication capabilities and equipment deserve detailed evaluation. Versatile cutting methods including laser, plasma, and saw handle different material types and thicknesses. Forming and bending capacity must match part complexity. Certified welders experienced in MIG, TIG, and robotic welding ensure joint quality. CNC machining accuracy supports tight tolerances when secondary operations are needed.
In-house secondary processes reduce lead times and logistical complexity. Powder coating, painting, heat treating, and final assembly offered under one roof simplify project management. Engineers avoid coordinating multiple vendors and reduce shipping between facilities.
Material sourcing and traceability protect against supply chain disruptions. A reliable network of material sources with full traceability from mill to finished part proves essential for regulated industries. Engineers should ask how suppliers verify material certifications and handle material substitutions.
Lead times and delivery performance affect project schedules. Consistent on-time delivery, flexible scheduling, transparent communication about production capacity, and experience with similar project sizes all contribute to reliable performance. Engineers should request references from customers with comparable projects.
Transparency and responsiveness build trust throughout the relationship. Open communication from initial quote through change orders prevents misunderstandings. Quick, clear answers from engineers and project managers keep projects moving. Suppliers who use technology for collaboration—sharing drawings, tracking job progress, and managing approvals—reduce miscommunication risks.
Total value beyond price should guide the final decision. The lowest quote is not always the best value. A 10-20% higher upfront price from a reliable supplier can avoid 2-3x higher total costs from rework, delays, and quality failures. Engineers should evaluate total cost of ownership and long-term partnership potential rather than focusing solely on initial pricing.
Supplier Evaluation Checklist
Capabilities and Equipment
A qualified fabricator owns equipment that matches precision enclosure requirements. Fiber laser cutters with automated loading handle sheets up to 60″ × 120″ and maximize material utilization through nesting software. ATC press brakes hold bend angle accuracy of ±0.5°, while manual press brakes serve tight-tolerance prototype work. Cutting and forming range from 0.020″ to 0.500″, with standard tolerances of ±0.005″.
Equipment Capability / Specification Fiber laser cutter Automated loading/unloading; nesting software; sheets up to 60″ × 120″ ATC press brakes Automatic tool changers; bend angle accuracy ±0.5° Manual press brakes Tight-tolerance prototype and low-volume work Cutting/forming range 0.020″ to 0.500″ (material-dependent) Standard tolerance ±0.005″, tighter values on request Engineers should confirm in-house laser cutting, CNC punching, forming, welding, hardware insertion, and finishing under one roof. Engineering support for DFMA and cost reduction adds further value.
Quality Standards and Certifications
Certifications separate serious fabricators from casual shops. ISO 9001:2015 demonstrates an effective quality management system with continuous process monitoring. AWS Certified Welding Fabricator status confirms welding proficiency. UL Certified NEMA Type 1 and 3R ratings verify enclosure performance. In-house powder coat testing—including ASTM D2794 impact, ASTM D3359 cross-hatch, and 50 MEK double rub—proves finish durability.
Certification/Standard Description ISO 9001:2015 Effective QMS with continuous improvement AWS Certified Welding Fabricator Proficiency in welding techniques UL Certified NEMA Type 1 / 3R Verified enclosure quality In-house powder coat testing ASTM impact, cross-hatch, MEK rub, gloss, thickness Lead Times and Communication
Lead times vary by complexity. CNC machining schedules may extend from one week to two or three weeks. A quote involving custom machining and external vendors once reached five weeks, while avoiding custom machining brought delivery back to the desired two-to-three-week range. Quick-turn flat parts can ship in as little as one day. Average custom fabrication projects range from a few days for small jobs to a few months for complex builds. Responsive communication during quoting predicts reliable performance during production.
Why Choose Qingdao Xuxiangtai for Precision Sheet Metal Enclosures
Full-Cycle Fabrication from Design to Delivery
Qingdao Xuxiangtai manages every stage of enclosure production under one roof. The company begins with engineering support and design optimization. Engineers create 3D and 2D drawings, conduct DFM reviews, and develop prototypes. This collaboration from concept through production eliminates handoff delays between vendors.
The fabrication team applies laser cutting, CNC punching, and CNC forming to achieve tight tolerances. Robotic press brake systems ensure consistent bend angles across every batch. CNC machining adds precision mounting provisions, threaded inserts, and custom hardware integration. MIG, TIG, and spot welding create robust assemblies that meet structural and aesthetic requirements.
In-house finishing covers powder coating, wet painting, and surface preparation. These processes deliver consistent appearance and corrosion protection. Assembly and integration transform fabricated enclosures into complete systems ready for installation.
Full-cycle fabrication delivers measurable advantages for buyers:
- Lower total landed cost through reduced cycle times and minimized waste
- Faster time-to-market with rapid prototyping and automated workflows
- Consistent compliance with ISO and industry standards
- End-to-end supply chain management for predictable quality
Quality Assurance and On-Time Fulfillment
Quality assurance at Qingdao Xuxiangtai operates as an integrated system rather than a final inspection gate. The company defines measurable quality standards aligned with industry norms and client requirements. Each fabrication step maps to critical control points where dimensional checks, material tests, and visual inspections occur. Staff receive thorough training on inspection techniques and issue reporting. Detailed documentation tracks inspection results, discrepancy handling, and corrective actions.
This structured approach reduces rework and sustains consistent output. Buyers receive precision sheet metal enclosures that meet specifications on the first delivery. On-time fulfillment follows from transparent scheduling and clear communication throughout production.
Precision sheet metal enclosures and low quantity fabrication give engineers a fast, cost-effective path from concept to functional parts. Engineers should match tolerances, materials, and processes to their application before requesting quotes. The supplier checklist helps compare fabricators on capability, quality, and lead time.
Engineers can submit their enclosure drawings to receive a no-obligation quote. The vendor’s engineering team reviews each RFQ for manufacturability and aims to respond within 24–48 hours via their request-a-quote page.
Take the next step by requesting quotes from Qingdao Xuxiangtai or consulting a fabrication expert to finalize the design.
FAQ
What is the minimum order quantity for custom sheet metal enclosures?
Qingdao Xuxiangtai accepts orders starting from a single prototype piece. Engineers can validate designs without committing to large production volumes.
How long does low quantity sheet metal fabrication take?
Standard lead times range from seven to fourteen days for small batches. Complex assemblies may require additional time for finishing and inspection.
What file formats do engineers need for requesting a quote?
Engineers should submit STEP files for 3D geometry and PDF drawings for dimensions and tolerances. This combination ensures accurate quoting and manufacturing.
See Also
Avoid Selecting Incorrect Aluminum Casting Methods Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.