- This topic is empty.
-
AuthorPosts
-
2026-10-16 at 3:52 pm #14759
Image Source:https://www.xuxiangtaimetal.com You need a custom metal manufacturing partner who simplifies sourcing. Qingdao Xuxiangtai delivers integrated fabrication across casting, forging, sheet metal processing, CNC machining, aluminum die casting, and surface finishing under one roof. Send your drawings for a quote within 24 hours. IATF 16949 and RoHS certifications back every order. With 20+ years of export experience, a 26,200 m² plant, and 460+ completed projects for 130+ international clients, you gain reliable global delivery without the usual headaches.
Key Takeaways
- Qingdao Xuxiangtai handles all metal manufacturing steps under one roof. This saves you time and money.
- You send your drawings and get a quote within 24 hours. The process is fast and simple.
- The company has certifications and a 95.3% on-time delivery rate. You can trust your order arrives on schedule.
Write a B2B English Company Introduction Article for US Industrial Buyers: Focus on Qingdao Xuxiangtai’s Metal Custom Manufacturing Capabilities
Qingdao Xuxiangtai Machinery Manufacturing Co., Ltd. operates as a full-service custom metal manufacturing partner for US industrial buyers. The company integrates casting, forging, sheet metal processing, CNC machining, aluminum die casting, and surface finishing under one roof. This integrated approach eliminates the need to coordinate multiple vendors. You gain fewer handoffs, faster lead times, and consistent quality from a single source. The sections below detail each manufacturing capability and explain how Qingdao Xuxiangtai applies these processes to meet your specifications.
Sheet Metal Processing for Precision Fabrication
Sheet metal processing forms the backbone of many industrial components. Qingdao Xuxiangtai delivers full-service precision sheet metal fabrication from cutting to final assembly. The process begins with laser cutting, which handles steel, aluminum, and stainless steel sheets up to approximately 6 mm thick with tolerances of ±0.1 mm. For thicker or exotic materials, waterjet cutting provides an alternative with tolerances of ±0.1–0.2 mm. CNC bending follows, achieving angle tolerances of ±0.5–1.0° and flat dimension tolerances of ±0.1–0.3 mm. Structural welding joins components with high-quality seams that withstand external stress. Stretching and stamping operations support high-speed volume production of thin-metal parts.
Material selection drives technique selection. You cannot anodize titanium, and you cannot deep draw brittle materials. Qingdao Xuxiangtai helps you match material to process from the start. The table below summarizes compatible materials and typical tolerances for common sheet metal operations.
Process Compatible Materials Typical Tolerances Laser cutting Steel, aluminum, stainless (up to ~6 mm) ±0.1 mm Waterjet Any metal, any thickness (best for thick/exotic) ±0.1–0.2 mm Press brake bending All metals ±0.5–1.0° angle; ±0.1–0.3 mm flat dimensions Deep drawing Ductile metals only (not brittle) ±0.1–0.2 mm Welding Steel, stainless, aluminum, titanium Strength varies by process (MIG < TIG < spot-weld for shear) Anodizing Aluminum only N/A Electroplating Primarily steel and copper alloys N/A Passivation Stainless only N/A Sheet metal fabrication suits flat, hollow, angular, or folded designs. CNC machining suits complex 3D features, deep pockets, and tight contours. The table below compares these two approaches across key dimensions.
Dimension CNC Machining Metal Fabrication Primary Method Subtractive—material removal from solid stock Forming and joining—cutting, bending, welding sheet/plate Raw Material Form Solid blocks, billets, bars, castings Flat sheet metal, plate, structural profiles Equipment Used CNC mills, lathes, drills, grinders Press brakes, laser cutters, welders, stamping presses Tolerance & Precision Extremely tight (±0.001″ to ±0.005″) Practical structural tolerances (±0.005″ to ±0.030″) Best-Fit Products Shafts, gears, valve bodies, precision fittings Frames, enclosures, brackets, structural assemblies Sheet metal fabrication offers lower per-part cost at scale. CNC machining costs more per part but is justified when precision or geometry complexity demands it. Qingdao Xuxiangtai operates both processes under one roof, so you receive the right method for each component without splitting your order across suppliers.
Casting Services for Complex Geometries
Casting services at Qingdao Xuxiangtai cover precision investment casting, sand casting, and die casting. Each method suits different geometries, volumes, and material requirements. Precision investment casting uses silicasol molding to achieve exceptional surface quality and tight tolerances directly from the mold. This process supports stainless steel, carbon steel, and alloy steels. It excels at thin walls around 2–3 mm, undercuts, internal cavities, and cored channels. Medical devices and industrial sensors benefit from this level of detail.
Sand casting provides a cost-effective solution for large structural iron components. The process accommodates large-format molds and produces heavy ductile iron parts that absorb operational shocks. QT450 ductile iron casting delivers structural integrity under heavy loads. Heavy industrial equipment manufacturers rely on this method for machine bases and large housings.
Die casting shapes aluminum and zinc components under high pressure. This method delivers net-shape parts with minimal secondary machining. High-volume production runs benefit from rapid cycle times. Thin-wall capability supports weight reduction goals in automotive and new energy vehicle applications.
The table below compares casting methods across criteria that matter for complex geometries.
Criteria Investment Casting Sand Casting Die Casting CNC Machining Thin wall capability Excellent (~2-3mm) Poor to fair (6mm+) Good for high-pressure alloys Limited by tool access/rigidity Undercuts / internal cavities Excellent (ceramic cores) Fair (sand cores, extra labor) Poor (die parting line limits) Very poor (tool cannot reach) Surface finish (as-cast) Very good Rough Good on exterior Excellent on reachable surfaces Dimensional tolerance Tight (±0.1-0.4mm) Loose Tight, limited alloys Tightest, costly on complex forms Tooling cost for complex shapes Moderate Low to moderate High (hardened steel dies) Low tooling, high cycle time Best-fit production volume Low to high Low to medium, large parts High volume only Low to medium, prototype-friendly Part consolidation potential High Moderate Moderate Low Casting quality standards matter for industrial applications. Qingdao Xuxiangtai holds IATF 16949 automotive quality management certification and RoHS environmental compliance certification. Components meet Class 150/300 international pressure rating standards. The table below outlines relevant certifications and their industrial applications.
Certification / Standard Full Name / Scope Industrial Application ISO 9001 Quality Management System – standardizes and continuously improves processes General manufacturing / all casting exports ISO 14001 Environmental Management – responsible environmental practices and waste reduction All industries with sustainability requirements ISO 45001 Occupational Health & Safety – employee safety and risk management Foundry operations across all sectors ASTM Technical standards for material chemical composition and mechanical strength General industrial castings requiring material performance guarantees API American Petroleum Institute standards for valves, pumps, and pressure-containing equipment Oil & gas and petrochemical applications IATF 16949 Automotive Industry Quality Management – quality, safety, and traceability Automotive engine, transmission, and structural castings Marine Approvals (Lloyd’s Register, DNV-GL, Bureau Veritas, ABS) Marine classification society approvals for saltwater, corrosion, and harsh marine environments Marine, naval defence, and offshore oil & gas Forging for Strength and Durability
Forging refines the grain structure of metal to provide superior fatigue resistance and tensile strength. The process realigns metal grains along the component’s stress lines. This grain flow alignment solves structural vulnerability in load-bearing parts. Forged components outperform cast or machined parts in high-stress applications.
The table below compares forging to casting across key criteria.
Criterion Forging Casting Precision & Complexity More limited in design complexity; often requires additional machining for tight tolerances Ideal for intricate geometries, thin walls, complex internal structures; near-net-shape minimizes post-processing Strength & Structural Integrity Typically stronger due to realignment of grain structure during deformation; edge in load-bearing and high-impact stress applications Can meet demanding performance standards with modern alloys and heat treatment, especially where precision is prioritized over brute strength Cost & Tooling Higher upfront tooling costs and more powerful equipment; cost-effective at scale for simple shapes More economical for low-to-medium production volumes and for parts costly to machine from forged stock Lead Time & Turnaround Quicker turnaround for simpler geometries once tooling is in place Can reduce lead times by minimizing machining steps and allowing faster iteration of complex designs Material Flexibility Limited material use flexibility compared to casting methods like investment casting Accommodates a broader range of alloys, including difficult-to-form or forge specialty materials Forged parts are stronger because the grain structure is realigned during deformation. This enhances tensile strength, fatigue resistance, and durability. Forging holds an edge in load-bearing applications and environments with high-impact stress.
The table below compares forged, cast, and machined parts across mechanical properties.
Property / Advantage Forged Parts Cast Parts Machined Parts Strength & Integrity Stronger due to optimized grain structure; can be lighter with less metal Weaker than forged; grain structure not optimized Lack grain flow of forging; significantly weaker Impact / Fatigue Resistance Tougher via grain flow and cold working; higher impact and fatigue resistance Lower toughness than forged Inferior fatigue resistance vs. forged Material Defects Highly homogeneous material via recrystallization and compaction; minimal porosity Prone to air bubbles/porosity, cold shuts, and segregation; costly to inspect No casting defects, but no grain-flow benefit Production Speed Faster than casting; stable, repeatable process with fewer steps Slower due to melting, pouring, solidification, breakout, and QC checks Slow and subtractive; one part at a time on costly machines Waste Minimization Limited secondary machining; small material removal vs. machining from billet/bar Near-net shape but can require overproduction due to quality losses High waste; chips disposal costly, especially for high-value alloys Lead Time Shorter lead times from order to delivery Longer due to multiple process steps Longer for high-volume production Best Use Cases High-volume production, waste minimization, enhanced mechanical strength, reduced lead time; automotive, aerospace, motorsport, firearms, agricultural/forestry, railroad Complex geometries, internal chambers/passages, material versatility Prototypes, custom/precision parts, low tooling cost, minimal lead time for tooling Forged aluminum shows approximately 26% higher tensile strength and 37% greater fatigue life than a similar cast alloy component. Billet can match or exceed cast strength but depends on alloy, temper, and design. Cast typically has the lowest strength due to porosity and shrinkage voids.
The table below compares billet aluminum, cast aluminum, and forged aluminum.
Factor Billet Aluminum Cast Aluminum Forged Aluminum Process Machined from solid stock Molten aluminum poured into mold Solid aluminum deformed under high pressure Strength Good (better than cast) Usually lower (depends on alloy/quality) Highest (exceptional tensile, yield, fatigue strength) Internal Structure Dense, wrought, uniform grain, very low defects May have porosity, shrinkage voids, inclusions Dense, aligned grain flow, minimal voids Design Freedom Very flexible for precise CNC features Excellent for complex 3D shapes and thin walls Moderate – limited by die design and metal flow Tooling Cost Low–Medium (no molds, just CNC) High for precision dies; lower for sand molds High (expensive die tooling and presses) Unit Cost High (labor/time heavy for large runs) Low per part at high volume Medium–High (cheaper at scale if volumes justify) Best For Prototypes, custom & precision parts Complex high-volume parts (housings, consumer goods) High-strength, safety-critical parts (suspension, aircraft) Surface Finish Excellent (smooth CNC finish) Variable (often rougher; may need sanding/polishing) Good, but often requires finishing/precision machining Industries that rely on forging include automotive, machinery, oil and gas, construction, power generation, heavy engineering, refineries, and power plants. These sectors demand high-strength, durable, and reliable components.
CNC Machining for Tight-Tolerance Components
CNC machining delivers subtractive manufacturing for ultra-tight tolerance metal components. Qingdao Xuxiangtai operates 5-axis CNC milling, CNC turning, composite machining, EDM, drilling, and tapping. These capabilities support complex geometries, symmetrical parts, hard metals, and mechanical fastening requirements. Medical, aerospace, and automotive industries depend on this precision.
Achievable tolerances vary by classification. The table below outlines typical ranges and applications.
Classification Typical Range Common Applications General purpose ±0.005″ to ±0.020″ Structural housings, brackets, non-critical fixtures Precision ±0.001″ to ±0.002″ Gears, shafts, fittings requiring closer fit High precision Below ±0.001″ (typically to ±0.0005″) Valve bodies, connector housings, surgical instruments, bearings Ultra precision Below ±0.0005″ (down to ±0.0001″ and tighter) Semiconductor equipment, optics, research instrumentation Ultra-precision machining can hold tolerances under ±0.0005″, roughly the thickness of a human blood cell. NASA’s White Sands Test Facility reports its CNC milling and turning machines commonly hold ±0.0002″ (±5 micrometers) on space-flight and repair components. Modern Machine Shop reports that many production shops regularly hold ±0.0002″ to ±0.0005″. Getting there requires linear scales and closed-loop feedback for real-time positioning, thermally stabilized environments to eliminate drift, specialized metrology such as CMM and laser interferometry for verification, and dedicated finishing operations separate from roughing.
Surface finish tolerance controls the texture of a machined surface. This texture is expressed as Ra (roughness average) in microinches or micrometers. ISO 21920-2:2021 supersedes the older ISO 4287 standard, changing the evaluation method so Ra is now calculated over the entire evaluation length. In the US, ASME B46.1-2019 remains the governing standard. Tighter surface finish requirements directly affect how parts seal, slide, or bond. These requirements typically demand additional finishing passes, grinding, or lapping.
Repeatability in CNC machining refers to the machine’s capacity to produce identical parts across multiple production runs while holding tight tolerances. This consistency is critical in sectors like aerospace, medical, automotive, and industrial manufacturing. Even slight deviations can impact performance, assembly, and safety. Dependable repeatability guarantees that each component fits properly and operates exactly as intended.
Several factors ensure repeatability. Precise programming, proper machine setup, quality materials, experienced machinists who carefully monitor the manufacturing process, tooling selection, machine calibration, and regular inspections throughout production all contribute. Robotic machine tending automates the repetitive but crucial task of loading and unloading CNC machines. While a CNC machine may be capable of holding tight tolerances, the surrounding setups must present each part consistently. Differences in loading, positioning, or part handling can introduce unnecessary variation. A CNC machine tending system follows the same programmed sequence every cycle, ensuring that part interactions with the machine remain consistent across multiple runs.
The table below compares local tools and branded tools for their impact on repeatability.
Aspect Local Tools Branded Tools Wear pattern Uneven Predictable Cutting edge sharpness Loses sharpness faster Stable cutting edges Tool geometry Varies between batches Precision-ground geometry Heat resistance Not specified Better heat resistance Impact on repeatability Causes dimensional shifts from part to part Ensures every component maintains the same tolerance throughout the production run The CNC machining process follows a defined sequence. Design review and engineering evaluation come first, with review of CAD files, tolerances, materials, and manufacturability considerations to improve machining efficiency and optimize production flow. Material selection follows, choosing the appropriate material based on performance requirements including strength, corrosion resistance, machinability, weight, and environmental exposure. CNC programming and toolpath development create machine programs that define cutting paths, tooling movements, spindle speeds, and machining operations. Machining operations use milling, turning, drilling, or multi-axis machining processes to create the final geometry. Secondary processes and finishing include deburring, surface finishing, coating, assembly preparation, or additional processing after machining. Inspection and quality control verify dimensions, tolerances, and overall quality requirements, ensuring repeatability and reducing the risk of production variability or rework.
Aluminum Die Casting for High-Volume Production
Aluminum die casting offers fast production cycles, tight tolerances, and smooth surface finishes. These characteristics make it highly efficient for high-volume manufacturing. The process delivers cost advantages at scale while supporting complex, customized part designs with minimal secondary machining.
The table below outlines the benefits of aluminum die casting for high-volume production.
Benefit How It Supports High-Volume Production Fast production cycles Short cycle times make aluminum die casting ideal for mass manufacturing and high-volume runs. Cost efficiency at scale Lower per-unit cost compared to sand casting or investment casting in large production runs. Tight tolerances Delivers precision components with minimal variation, ensuring consistent quality across large batches. Smooth surface finish Reduces secondary machining and finishing costs, streamlining high-volume output. Design flexibility Supports complex, customized part designs with minimal secondary machining. Lightweight and durable parts Produces lightweight parts without sacrificing strength, valuable for automotive and EV mass production. Corrosion resistance and recyclability Aluminum offers strength, corrosion resistance, and recyclability, benefiting long-term high-volume programs. Aluminum die casting produces lightweight and durable parts without sacrificing strength. The material offers a good strength-to-weight ratio, great resistance to corrosion, excellent electrical conductivity, and full recyclability. Rapid production enables a high volume of parts to be produced quickly and more cost-effectively than alternative casting processes.
Tooling costs and lead times vary by casting process. The table below provides typical ranges.
Process Tooling Cost Range Build Lead Time Green sand — wooden pattern $800 – $3,000 1–3 weeks Green sand — aluminum pattern + core boxes $4,500 – $14,000 3–6 weeks Resin / no-bake sand — cast iron pattern $6,000 – $20,000 4–8 weeks Shell mold — heated cast iron pattern $8,000 – $30,000 5–9 weeks Lost foam — aluminum foam tooling $15,000 – $60,000 6–12 weeks Investment casting — aluminum wax die $3,000 – $25,000 3–7 weeks Investment casting — hardened steel wax die $12,000 – $45,000 6–10 weeks Permanent mold — gray iron or H13 mold $12,000 – $45,000 6–10 weeks High-pressure die casting — H13 die $25,000 – $150,000+ 8–16 weeks Centrifugal casting — steel mold $10,000 – $50,000 6–12 weeks A die casting die takes molten aluminum at 660–700 °C injected at 40–100 MPa and must survive that thermal shock tens of thousands of times. That calls for premium H13 tool steel, vacuum heat treatment to 44–48 HRC, deep EDM or high-speed machining of the cavity, conformal cooling lines, and a bolster stiff enough to resist 800–4,000 tons of clamping force without flashing. You are not paying for shape; you are paying for survival under load. That gap is the single biggest driver of casting tooling cost variation between processes.
NADCA practice puts aluminum high-pressure die life at roughly 80,000–150,000 shots before major refurbishment. Magnesium falls in a similar band. Zinc hot-chamber tooling reaches 500,000 to over 1,000,000 shots. Zinc melts at 420 °C instead of 660 °C, so the thermal fatigue per shot is dramatically lower.
A 2-cavity H13 die quoted at $74,000 serves as a representative example. Program volume is 30,000 castings per year, so 15,000 shots per year. Expected life before major refurbishment is 120,000 shots.
The die casting process follows a defined sequence. Requirement review, DFM, tool design, steel and component procurement, machining, assembly, trial, measurement, correction, product approval, production, secondary operations, inspection, packing, and transport all occur in order. The process delivers first trial, approval-ready sample submission, and production shipment.
Surface Finishing to Meet Your Specs
Surface finishing enhances corrosion resistance, wear resistance, and aesthetic appeal. Qingdao Xuxiangtai offers anodizing, powder coating, electroplating, Dacromet coating, bead blasting, and passivation. Each finish serves specific environmental and functional requirements.
The table below outlines surface finish characteristics for common methods.
Finishing Method Surface Finish Characteristics As Machined Minor tool marks; standard roughness (Ra) of 3.2μm, refinable to 1.6, 0.8, or 0.4μm Bead Blasting Matte finish with light texture, mainly for visual purposes Powder Coating Wear- and corrosion-resistant finish with higher impact resistance; applicable to any metal and available in many colors Anodizing Type II (Clear or Color) Corrosion-resistant ceramic layer on aluminum or titanium; can be dyed different colors Anodizing Type III (Hardcoat) Stronger corrosion-resistant ceramic layer than Type II; can also be dyed different colors Finish selection depends on environmental exposure, appearance requirements, durability needs, and budget constraints. General guidance suggests choosing finishes with high corrosion resistance for outdoor applications. Opt for finishes with versatile color and texture options when aesthetics are critical.
Surface finishing processes fall into three categories. Material removal includes surface grinding, honing, lapping, and polishing, which progressively refine the surface. Deburring removes edge burrs. In CNC machining, the achieved finish depends on tool geometry, feed, speed, rigidity, and tool wear. Mechanical texturing includes bead blasting, which produces a uniform matte non-directional texture, typically as preparation for coating or for cosmetic uniformity. Coating and conversion includes anodizing, powder coating, plating, and painting. These processes add a layer that changes corrosion resistance, appearance, and sometimes electrical conductivity. The pre-treatment finish matters as much as the coating.
Surface roughness affects corrosion resistance significantly. Rough surfaces trap moisture, salts, and contaminants in microscopic valleys, creating localized corrosion cells that lead to pitting or crevice corrosion. Smoother finishes from polishing and buffing reduce accumulation sites and improve corrosion resistance. Stainless steel relies on a chromium oxide film for corrosion resistance. Mechanical polishing can improve film uniformity, but aggressive grinding or contamination with iron particles can disrupt the passive layer and initiate rust. Passivation removes free iron and promotes a more stable oxide layer, especially after cutting, welding, or machining. Electropolishing creates an ultra-smooth surface, reduces micro-crevices, and enriches chromium at the surface, strengthening the passive layer.
Coatings and plating create physical barriers. Powder coating, anodizing, and galvanization protect the underlying metal. Galvanization adds a sacrificial zinc layer. However, scratches, pinholes, or uneven coverage can allow corrosion to propagate beneath the coating. Weld zones may contain oxides, heat tint, and residues that reduce corrosion resistance. Pickling and passivation restore protective properties by removing heat tint and depleted chromium areas. Marine or coastal environments favor smoother, chemically treated finishes. Industrial acid or pollutant exposure benefits from coatings plus proper finishing. Regular cleaning and inspection prevent contaminant buildup and coating damage. Advanced finishing such as electropolishing may cost more upfront but can lower maintenance needs and extend service life, making it cost-effective over time.
Several finishing methods provide specific corrosion protection. Electrocoating (e-coating) immerses parts in an electrolyte solution containing paint or primer. Electrically charged coating deposits on the metal surface and is widely used for corrosion resistance, especially in automotive applications. Electroplating uses an electrolyte solution with metals such as chromium, nickel, or zinc and an electric current to deposit a metal coating. This increases corrosion resistance, provides protection, and improves aesthetics. Anodizing is an electrochemical process, typically for aluminum, that creates a natural oxide layer acting as a protective coating. This improves wear and corrosion resistance. Powder coating provides a durable protective finish that can improve corrosion resistance and appearance. Thermal spray coating applies protective material to a surface to improve properties such as corrosion resistance. Before coating, contaminants must be removed and the surface roughened or chemically altered so the coating bonds strongly. Poor preparation can undermine corrosion protection.
Research on butt-welded stainless steel and aluminum alloys shows that surface quality after finishing strongly affects corrosion resistance. Residual stresses influence thermodynamic instability. Tensile residual stresses promote stress corrosion cracking, especially at stress concentrators in corrosive environments. Compressive residual stresses can slow corrosion cracking and improve corrosion fatigue resistance. The study compares traditional grinding with innovative post-weld finishing and evaluates surface roughness, residual stresses, microstructural changes, and microhardness to determine which finishing approach best improves durability and longevity in corrosive service.
How Qingdao Xuxiangtai Makes Customization and Quoting Simple
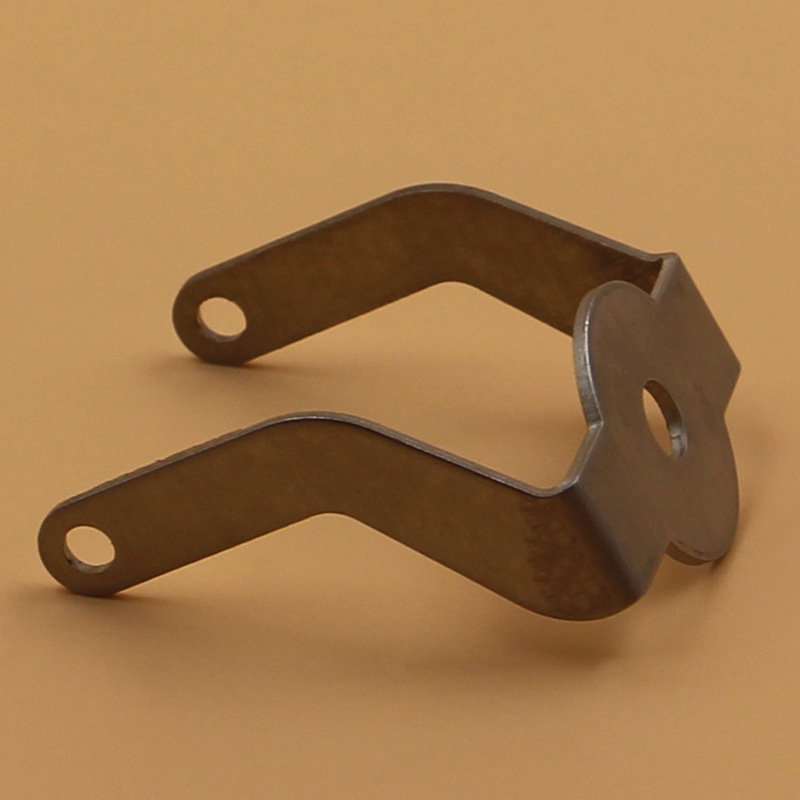
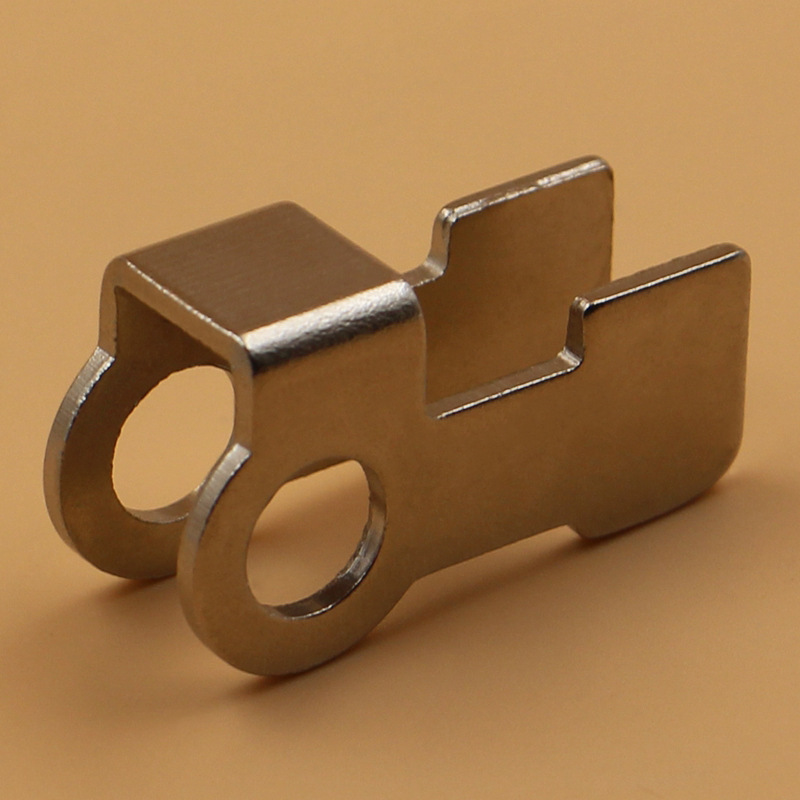
You send a drawing. You receive a quote. That exchange sounds straightforward, yet many buyers struggle with suppliers who request endless clarifications, miss deadlines, or deliver parts that fail inspection. Qingdao Xuxiangtai built its quoting and delivery process around one goal: remove friction from your sourcing experience. This section explains how the drawing-based quotation works, what delivery timelines you can expect, and why US industrial buyers keep returning to this partner.
How the Drawing-Based Quotation Process Works
The quotation process starts with your technical drawing. You submit a 2D drawing, a 3D model, or both. Qingdao Xuxiangtai reviews the file and responds with a detailed quote. The company accepts drawings in standard formats including PDF, DWG, STEP, and IGES. You do not need to prepare special documentation beyond what your engineering team already produces.
A complete drawing accelerates the quoting process. Missing information forces back-and-forth exchanges that delay your project. The checklist below covers the essential elements Qingdao Xuxiangtai reviews before pricing your part.
- Title block and revision currency. Confirm that the RFQ, filename, title block, model, and customer-approved revision match. Any mismatch requires clarification before pricing.
- Geometry completeness. Ask whether a machinist or fabricator can define the part without guessing. Missing views, incomplete dimensions, unclear sections, or ambiguous bend and weld details affect programming, setup, cycle time, fabrication labor, and risk allowance.
- GD&T and datum strategy. Test whether the shop can fixture, produce, and inspect the requirement with available equipment. An inaccessible datum, unclear tolerance relationship, or undefined surface condition may require additional fixtures, setups, probing, inspection, machine capability review, or outside processing.
- Material and stock callout. Confirm the exact alloy, temper, thickness, heat treatment, certification, and grain direction where specified. Missing conditions should trigger a purchasing clarification.
- Operations and finishing clues. Convert every note into a physical action. Threads, counterbores, weld preparations, masking, anodize, powder coat, passivation, and inspection requirements belong in the routing. Include cycle time, tooling, outside services, transport, finishing labor, and post-process inspection.
- BOM and package consistency. Compare the assembly, detail drawings, BOM, specifications, RFQ correspondence, and revisions. Quantity conflicts, stale files, missing hardware, or incompatible finishes require package-level clarification.
- Final margin sanity check. Put the proposed route beside machine time, setup hours, inspection time, outside-service costs, material exposure, and the promised delivery date. Write down any assumption that the quote depends on before sending it.
Each drawing clue translates into a routing line item, a cycle-time factor, and a pricing lever. The table below shows how Qingdao Xuxiangtai maps drawing features to production steps.
Drawing Clue Routing Line Item Cycle-Time Factor Pricing Lever Alloy, temper, or certified material Purchase and incoming verification Availability, stock size, certification handling Material markup, purchasing labor Threaded holes Drill, tap or thread mill, inspect Hole count, depth, tool access Machine time, tooling, inspection Counterbores or countersinks Secondary hole operation Tool changes, depth control, access Setup and cycle allowance Weld preparation Cut, bevel, fit, weld, clean Joint length, distortion, access Fabrication labor, fixtures, inspection Anodize, powder coat, or passivation Outside processing and post-finish check Vendor queue, masking, transport Outside-service price, handling, lead time Masking or selective finish Mask, process, unmask, inspect Surface area and feature protection Manual labor, risk allowance Material selection affects both pricing and lead time. Qingdao Xuxiangtai stocks or sources a wide range of metals to match your specifications. The table below lists available material grades for drawing-based quotation.
Material Category Available Grades Aluminum 1100-H14, 5052-H32, 6061 Copper 101, C110, C110 H02, 260 (Brass) Bronze 220, 510 Stainless Steel 301, 304, 304 #4 brushed, 304 #8 mirror polish, 316/316L, 316 #4 brushed Steel 1018 (Low Carbon), 1045 (Hot Rolled), A569/ASTM A1011 (Hot Rolled), AZ55 Galvalume, A653 Galvanized, 1095 Spring Steel, A36, A36 pickled and oiled, A366/1008 Nickel Alloys Inconel 625, Nickel Alloy 200, Nickel Alloy 400 Titanium Grade 2, 6AI-4V (Grade 5) Before you finalize your drawing package, run a consistency check across all files. The questions below help you catch problems before they reach the quoting stage.
- Revision match: Does the assembly revision agree with every detail drawing used for pricing?
- Quantity match: Does the BOM agree with the RFQ quantity and any customer note?
- Geometry match: Does the drawing reference a feature, model, or mating part that still exists?
- Requirement match: Do notes, specifications, and inspection requirements agree across files?
- Hardware match: Are purchased components, fasteners, inserts, and finishing requirements included?
Practical rule: If a drawing requirement can’t be assigned to a routing step, a responsible person, or a quote line, it hasn’t been reviewed deeply enough.
Qingdao Xuxiangtai responds to quotation requests within 2 hours during business hours. The engineering team reviews your drawing, identifies any missing information, and prepares a detailed quote. You receive pricing, lead time estimates, and any assumptions the quote depends on. This transparency lets you compare quotes accurately and avoid surprise costs later.
Delivery Service and Timeline Expectations
Delivery timelines depend on your chosen shipping method, order volume, and destination. Qingdao Xuxiangtai ships from its Qingdao facility to US destinations through multiple logistics channels. You select the method that balances speed and cost for your project.
The table below outlines typical delivery timelines from China to the US.
Shipping Method Typical Delivery Timeline (China to US) Regular Post (airmail/EMS) 1–2 weeks Express Courier (DHL, FedEx, UPS, TNT) ~3 days (premium services may deliver overnight) Standard Air Freight 8–10 days Express Air Freight 2–3 days faster than standard air freight (approx. 5–8 days) Sea Freight (door-to-door) 30–40 days Expedited Sea Freight Faster than standard sea freight; may be competitive with air freight lead times Express courier services deliver door-to-door in 2 to 5 days, including customs clearance and tracking. Each package has a 150 lb limit, which suits small tools, replacement parts, or urgent items. Air freight handles urgent parts, small precision equipment, or high-value machinery. Cargo planes can carry up to 20 tons but with tight size limits. Multimodal options combine sea freight for main shipments and air freight for urgent parts. Rail from West Coast ports can reduce inland delivery costs.
Total delivery timeline includes ocean transit plus customs clearance. Add 3–5 days for US customs processing and documentation review. Inland trucking adds additional days for door delivery. You can choose port pickup, terminal delivery, or door-to-door service.
Customs clearance and logistics planning directly affect your delivery schedule. Traditional freight can face delays from customs clearance, poor routing, and limited visibility. Small shipments often receive lower priority. Qingdao Xuxiangtai mitigates these risks through customs-ready documentation, including automated commercial invoicing and harmonized code support. This preparation reduces clearance delays and keeps your shipment moving.
A Berlin-based electric mobility startup ordered 20 custom stainless steel brackets from China. Production began within 24 hours. Parts shipped by day four with express tracking. Final delivery occurred on day seven. This example shows how integrated customs and logistics planning shortens delivery schedules for international metal manufacturing orders.
Qingdao Xuxiangtai maintains a 95.3% on-time delivery rate. The company responds to inquiries within 2 hours and maintains a 25% reorder rate. These metrics reflect consistent performance across hundreds of international orders.
Why US Buyers Choose Qingdao Xuxiangtai
US industrial buyers face a crowded field of overseas suppliers. Many promise low prices and fast delivery. Few deliver both consistently. Qingdao Xuxiangtai stands apart through verified performance, transparent communication, and integrated capabilities that reduce your vendor management burden.
The company holds IATF 16949, ISO 9001, and RoHS certifications. These certifications validate quality management systems, automotive-grade production standards, and environmental compliance. Qingdao Xuxiangtai also holds Verified Supplier Pro status and maintains a 5.0/5.0 supplier rating.
The table below summarizes key performance metrics.
Metric Value On-time delivery rate 95.3% Response time ≤2 hours Reorder rate 25% Facility size 26,200 m² Completed projects 460+ International clients 130+ Qingdao Xuxiangtai offers multiple customization approaches to match your project needs. You can choose drawing-based customization, sample-based customization, graphic processing, or customized on demand. The company provides investment casting, die casting, sand casting, and automotive parts manufacturing under one roof.
An outdoor IoT communication device manufacturer needed robust, corrosion-resistant casting components that could withstand extreme temperatures, humidity, and UV exposure. Qingdao Xuxiangtai recommended a specialized aluminum alloy with advanced anodizing surface treatment. The company provided sample-based customization for iterative design refinements. The resulting components extended device lifespan and contributed to a 15% reduction in warranty claims related to environmental damage. Efficient production and quality control supported cost-effective volume manufacturing and a reliable supply chain.
Quality assurance extends beyond certifications. Qingdao Xuxiangtai applies a multi-stage verification protocol across every order. The company requires material certifications including mill test reports, first-article inspection reports with dimensional validation, and periodic destructive testing. For critical components, you can request third-party inspection at the supplier’s facility. Production part approval process documentation provides comprehensive process validation. Virtual or physical supplier audits verify stated capabilities.
Cost advantages come from integrated manufacturing. Qingdao Xuxiangtai performs casting, forging, sheet metal processing, CNC machining, aluminum die casting, and surface finishing in-house. You avoid markups from subcontractors and reduce coordination overhead. Sample pricing ranges from $0.10 to $101 depending on part complexity and material. Production pricing scales favorably with volume.
The table below compares Qingdao Xuxiangtai to other suppliers on response time.
Company Name Review Score Response Time Qingdao Xuxiangtai Machinery 5.0 ≤1h Foshan Zeren Precision Casting 5.0 ≤1h Dongguan Dingqiao Metal 5.0 ≤2h Linyi Hongsheng Foundry 5.0 ≤3h Jining Wabon Precision Metal 5.0 ≤3h US buyers choose Qingdao Xuxiangtai for the combination of speed, quality, and simplicity. You send a drawing. You receive a quote within hours. You approve the quote and receive parts on schedule. The process works because the company controls every manufacturing step and communicates clearly at each stage.
Cover Sheet Metal Processing and Beyond: One Partner for Every Metal Process
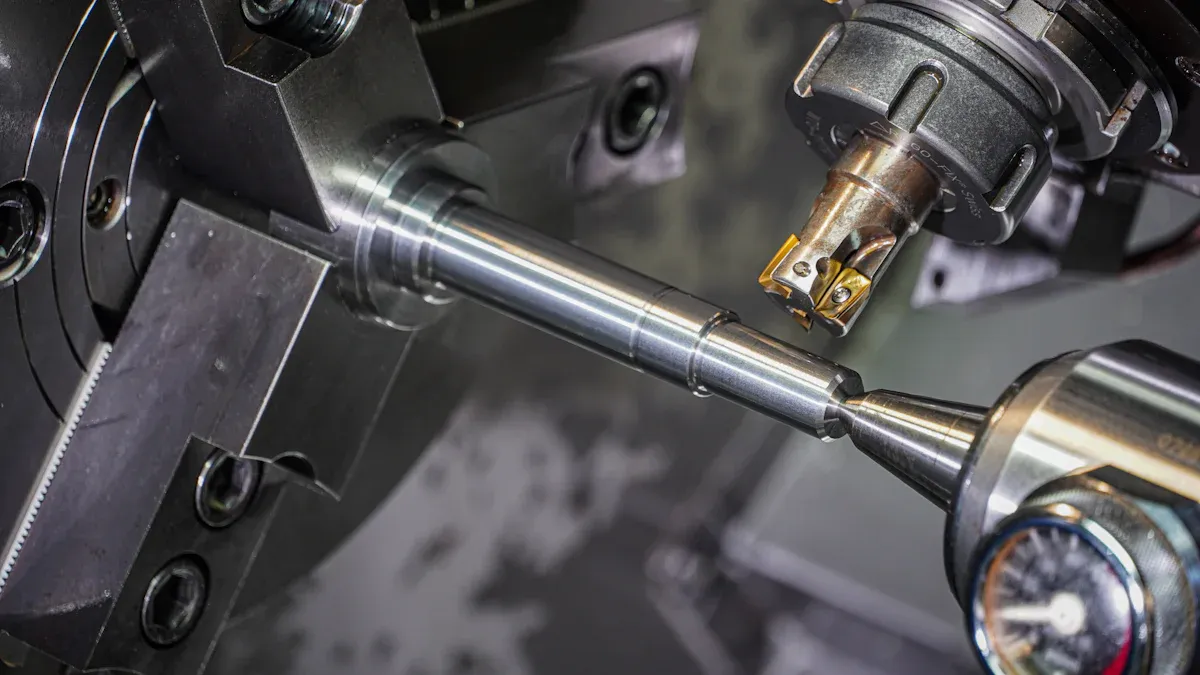
Image Source: https://www.xuxiangtaimetal.com Integrated Full-Process Support from Design to Assembly
You gain a single point of accountability when you partner with Qingdao Xuxiangtai. The company handles design review, mold making, prototyping, volume manufacturing, and final assembly under one roof. This integrated approach eliminates the friction of coordinating multiple vendors. You avoid shipping delays between suppliers. You reduce administrative burdens. You receive consistent quality from raw material to finished assembly.
The benefits of this model extend beyond convenience. Faster turnaround times result from eliminating hold-ups between production stages. Cost efficiency improves through consolidated logistics and reduced handling. Design and engineering support helps you refine concepts before production begins. Prototyping capabilities let you validate designs quickly and avoid costly redesigns.
Quality Assurance Across Every Manufacturing Stage
Quality assurance at Qingdao Xuxiangtai follows a proactive approach. The company implements standardized procedures and maintains detailed documentation throughout production. Statistical process control monitors variations continuously. In-process inspections catch deviations early. Non-conforming materials are quarantined immediately to prevent contamination of final products.
Every order includes material certifications, first-article inspection reports, and dimensional validation. For critical components, you can request third-party inspection or production part approval process documentation. The company holds IATF 16949, ISO 9001, and RoHS certifications. These credentials validate quality management systems and environmental compliance across every manufacturing stage.
Industries Served and Proven Results
Qingdao Xuxiangtai serves diverse industries with specialized requirements. The table below outlines key sectors and their manufacturing needs.
Industry Key Requirements Automotive IATF 16949 compliance, tight tolerances, high-volume production Aerospace Certified processes, material traceability, complex geometries Medical Devices Precision machining, premium surface finishes, regulatory compliance Renewable Energy Corrosion resistance, durable components, large-scale fabrication Heavy Industrial Equipment Vibration damping, structural integrity, shock absorption The company has completed over 460 projects for more than 130 international clients. A healthcare equipment manufacturer achieved premium cosmetic finishes and precise mechanical tolerances on smart medical beds. A heavy machinery developer gained high vibration damping in machine tool setups. These results demonstrate the company’s ability to deliver proven solutions across demanding applications.
Qingdao Xuxiangtai covers every metal process you need: sheet metal processing, casting, forging, CNC machining, aluminum die casting, and surface finishing. You send drawings, receive a fast quote, and get reliable delivery. With 20+ years of export experience, a 26,200 m² plant, and 460+ projects for 130+ clients, the company simplifies your sourcing. Send your drawings today for a custom quote.
FAQ
What file formats do you accept for custom metal manufacturing quotes?
You can submit PDF, DWG, STEP, and IGES files. Qingdao Xuxiangtai reviews your 2D drawings or 3D models and responds with a detailed quote within 2 hours during business hours.
How long does delivery take from China to the US?
Delivery timelines vary by shipping method. Express courier takes about 3 days. Air freight takes 8–10 days. Sea freight takes 30–40 days. You choose the option that fits your schedule.
What certifications back your custom metal components?
Qingdao Xuxiangtai holds IATF 16949, ISO 9001, and RoHS certifications. Components meet Class 150/300 pressure rating standards. Every order includes material certifications and dimensional validation reports.
See Also
Avoid Making Incorrect Decisions When Selecting Aluminum Casting Methods Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.